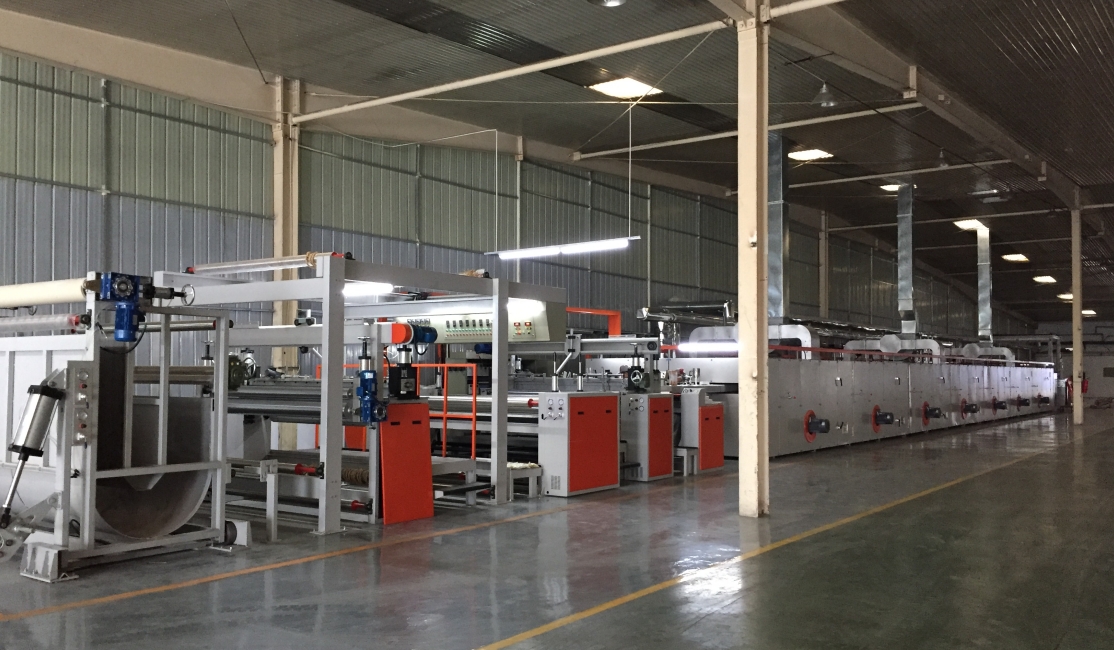
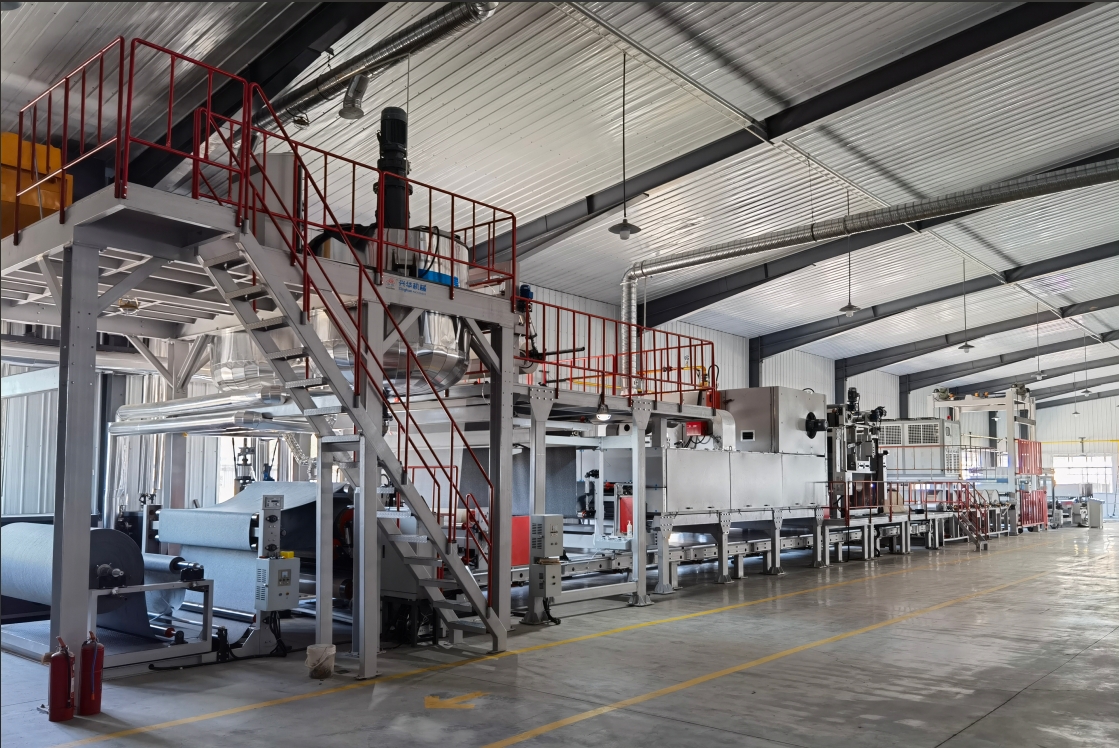
Pre-coating line for woven and tufted carpet backing (pre-coating and drying) to prepare for subsequent PVC / bitumen / TPO coating.
| Model / series | FH-220-420 |
|---|---|
| Nominal width | 200-400cm |
| Machine speed | 3-18m/min |
| Typical running speed | 10-13m/min |
| Heat source | thermal oil 15%; natural gas 80%; steam 5% |
| Oven | Configured to customer needs |
Pre-coating line for woven and tufted carpet backing (pre-coating and drying) to prepare for subsequent PVC / bitumen / TPO coating.
This line pre-coats and dries woven and tufted carpet backing so the web is ready for a later PVC, bitumen, or TPO coat (published USE). It is not the final tile-backing host.
Typical position: greige infeed → pre-coat → dry → cool / accumulate → feed the main PVC or bitumen/TPO line. Pre-coat weight and dry-band stability affect fiber lock and how evenly the main coat sits.
Oven is configured to customer needs. Heat-source options follow the TECH mix (thermal oil / natural gas / steam).
Model FH-220-420: published pre-coat series covering a wide width band.
Nominal width 200–400 cm: match greige usable width and the downstream host width—do not order a pre-coat wider than the plant can feed into the main line without rework.
Machine speed 3–18 m/min; typical running speed 10–13 m/min. Pre-coat is often run faster than the plasticizing host; final coupling speed is set in the whole-line proposal, not by taking the mechanical max alone.
Electro-hydraulic servo in carpet coating (publication CN206111703U): public text describes servo control for carpet coating-process motion. On a pre-coat line this is relevant where coat weight and drive sync need tighter tracking into the dryer—exact hardware follows the quotation.
For main-coat head and oven patents, see the PVC and bitumen/TPO product pages. We highlight only process-linked public directions here; no patent wall on the site.
Common flow: this pre-coat → PVC tile line or bitumen / TPO tile line → continuous cutting (if separate) → packaging.
If greige already arrives with a qualified pre-coat, the host can lead—but write pre-coat quality into incoming standards. When inquiring, send greige type/width, target pre-coat weight band, heat source, and which main chemistry follows.
Usually a fit: woven or tufted greige that will later take PVC or bitumen/TPO; new plants wanting a dedicated pre-coat dry section; width needs inside the published 200–400 cm band.
Usually another page: final PVC or bitumen host capability (carpet-01 / carpet-02); cutting-only (carpet-11); demanding locked main-coat peel values with no greige or paste data.
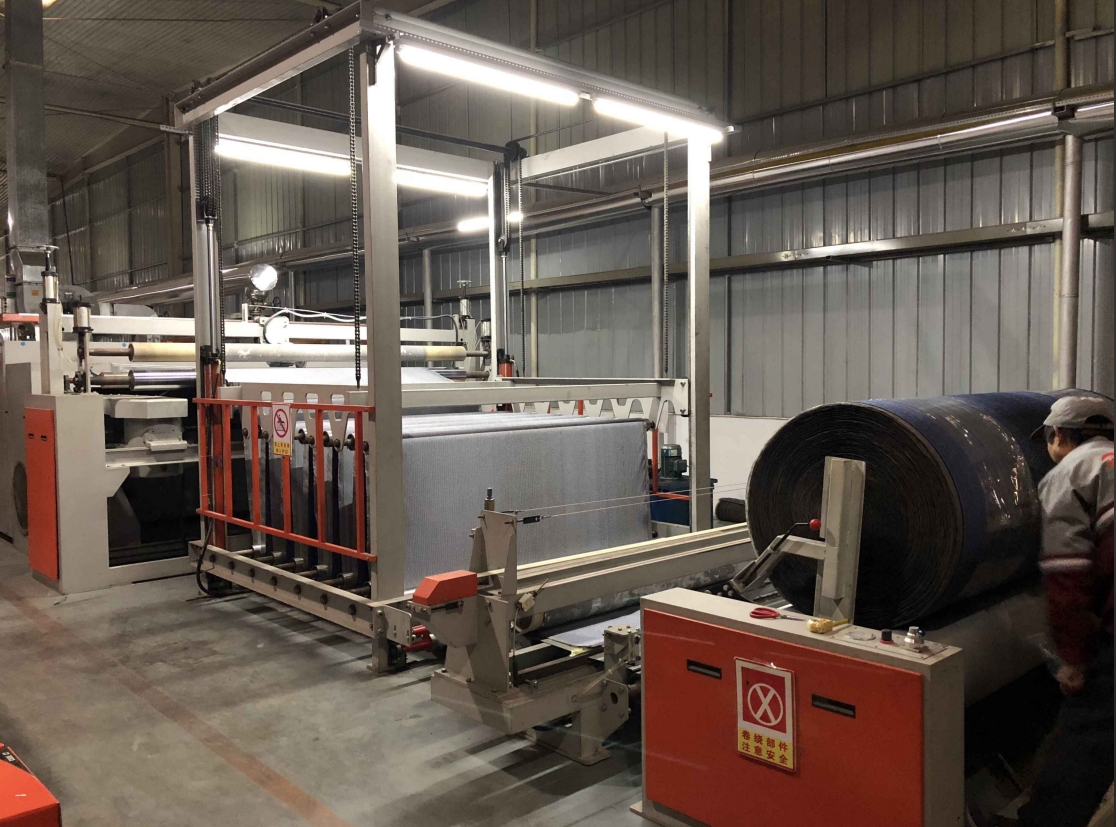
Production line for PVC carpet tiles - backing coating, plastication and automatic cutting for tufted or needle-punched, nylon or polypropylene carpets, producing 50x50, 50x100, 25x100, 100x100 and polygonal tiles.
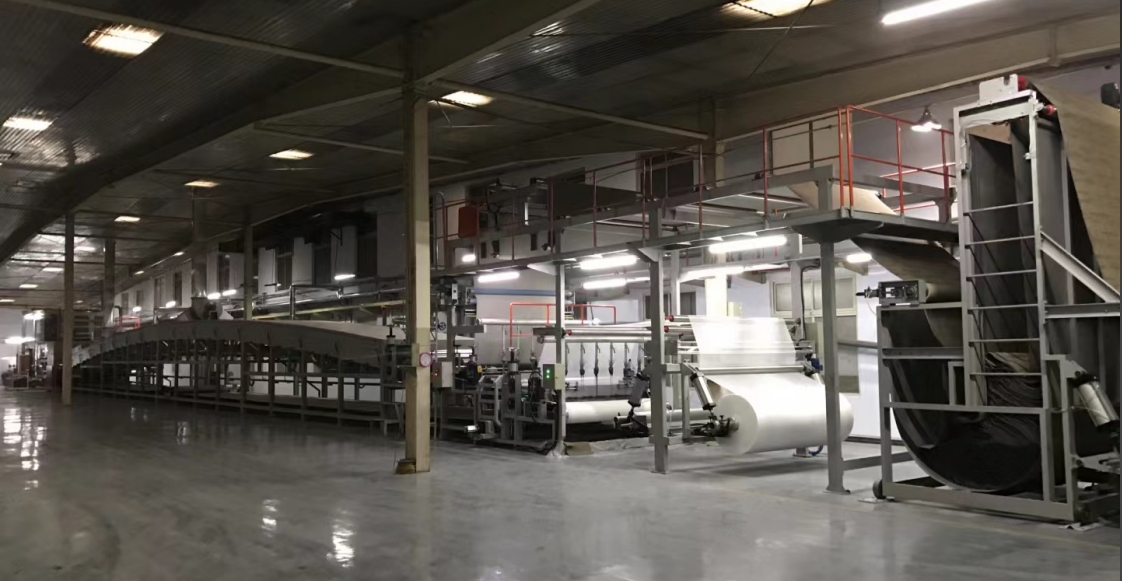
Production line for bitumen / TPO carpet tiles - back coating with bitumen/TPO, backing, cooling and automatic cutting for tufted or needle-punched carpets, available in slitting or fully automatic continuous production.
A: TECH on this page: model FH-220-420; nominal width 200–400 cm; machine speed 3–18 m/min; typical running speed 10–13 m/min; oven configured to customer needs; heat-source mix thermal oil / natural gas / steam as published percentages. Full fields are in the TECH table—ignore any legacy FAQ text about tile piece counts; those are not on this TECH table.
A: No. USE states this line prepares backing for subsequent PVC / bitumen / TPO coating. Final tile backing, plasticizing or bitumen cool, and tile formats live on the host pages.
A: Pre-coat dry loads often allow a higher stable window (published typical 10–13 m/min here vs 5–6 m/min typical on carpet-01). Whole-line rhythm is still gated by the slower plasticizing or cooling section—plan buffers or matched speeds in the proposal.
A: Not always. It is strongly useful for new plants or greige with weak fiber lock. If incoming material already meets a written pre-coat standard, start with the host and keep pre-coat as a later module.
A: Greige type and usable width, target pre-coat weight band, heat source, dryer length limits in the building, which main chemistry follows (PVC vs bitumen/TPO), and target shift output. Call +86 510 83397635 / +86 510 83382635 or email info@xhmachinery.com.