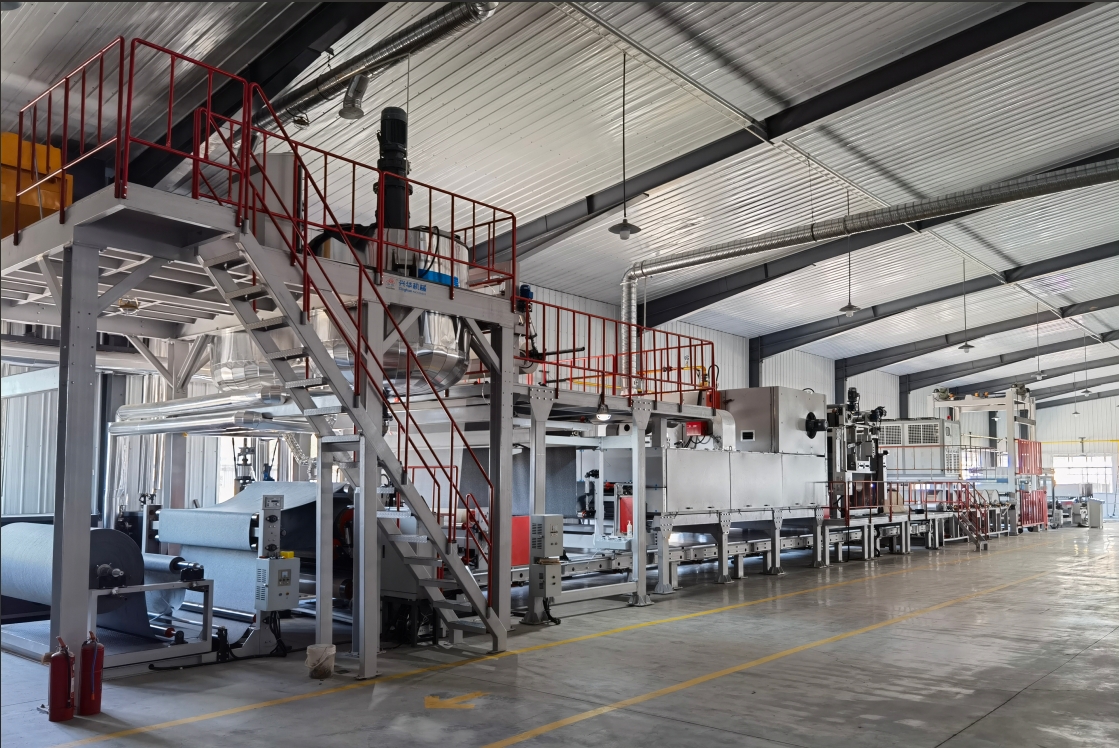
Production line for bitumen / TPO carpet tiles - back coating with bitumen/TPO, backing, cooling and automatic cutting for tufted or needle-punched carpets, available in slitting or fully automatic continuous production.
| Model / series | FH-220 |
|---|---|
| Nominal width | 200cmadjustable |
| Machine speed | 1-12m/min |
| Typical running speed | 5-7m/min |
| Heat source | thermal oil 15%; natural gas 80%; steam 5% |
| Oven | Configured to customer needs |
| Oven temperature | 100-200℃ automatic control |
| Cooling temperature | 20-60℃ automatic water cooling |
| Main power | ≈45KW (automatic ≈60KW) |
| Production mode | Slitting / fully automatic continuous |
Production line for bitumen / TPO carpet tiles - back coating with bitumen/TPO, backing, cooling and automatic cutting for tufted or needle-punched carpets, available in slitting or fully automatic continuous production.
The line applies bitumen or TPO back coating to tufted or needle-punched carpet, adds backing as required, cools, then cuts tiles. Published USE lists slitting or fully automatic continuous production.
After coat and backing, the web must cool into a stable state before cutting. TECH publishes cooling temperature 20–60℃ with automatic water cooling—set against compound and line speed in commissioning, not as a single universal setpoint.
Oven band 100–200℃ automatic control; oven length/chambers configured to the order. Heat-source options match the TECH mix (thermal oil / natural gas / steam).
Model FH-220: published bitumen/TPO tile series. Nominal width 200 cm adjustable—confirm greige usable width.
Machine speed 1–12 m/min; typical running speed 5–7 m/min. Top of the mechanical band is not a guaranteed process rate for every compound.
Main power ≈45 KW; automatic continuous configuration ≈60 KW on this page. Production mode: choose slitting or fully automatic continuous when you inquire—tooling and downstream handling differ.
Asphalt composite coating head (publication CN219723533U): public text describes a composite coating head aimed at asphalt (bitumen) application on carpet backing lines—useful context when comparing knife/head layouts for bitumen programs. Exact head on your order follows the model quotation.
Electro-hydraulic servo in carpet coating (publication CN206111703U): describes servo control during carpet coating so process motion can track setpoints more closely. Not a claim that every shipped axis uses the same hardware as the drawings.
Patent notes are technical directions from public texts for overseas buyers. No full patent wall on the site; ask sales for a longer list. Numbers are not a statement of present legal force.
This machine: bitumen or TPO route with published cooling band and slitting / continuous modes.
PVC Carpet Tile Production Line: PVC coat → plasticize on Teflon belt → cut; different chemistry and oven story.
Upstream: pre-coating. Downstream: continuous cutting (if separate) and packaging.
Usually a fit: tufted or needle-punched greige for bitumen or TPO tile backing; need for published cooling control; slitting or continuous tile output.
Usually another page: PVC-only programs (carpet-01); no compound or greige data yet locking peel/dimensional acceptance; non-tile roll coating without cutting.
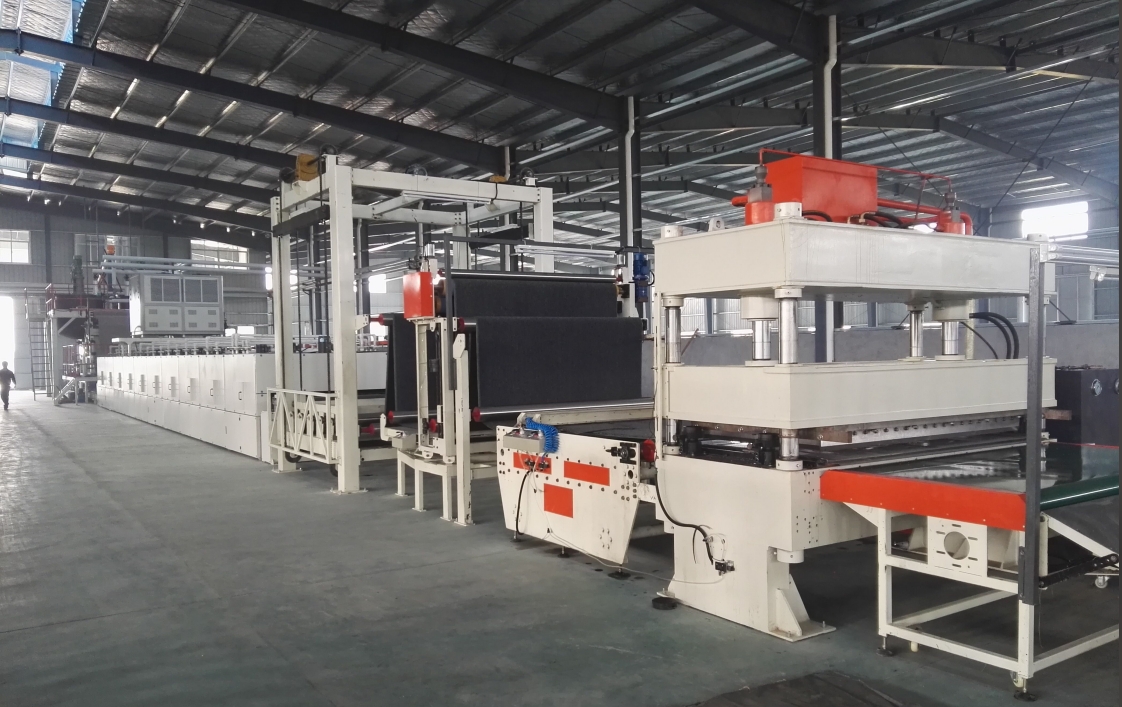
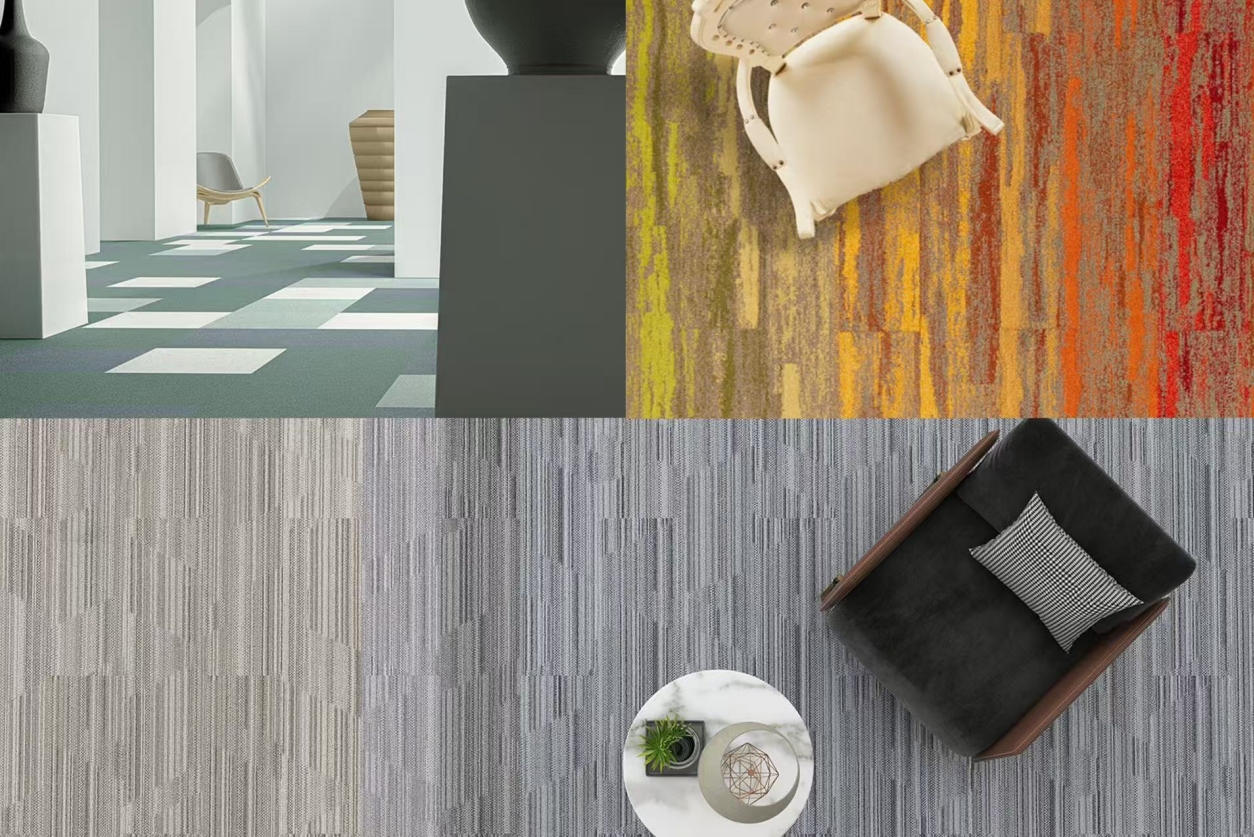
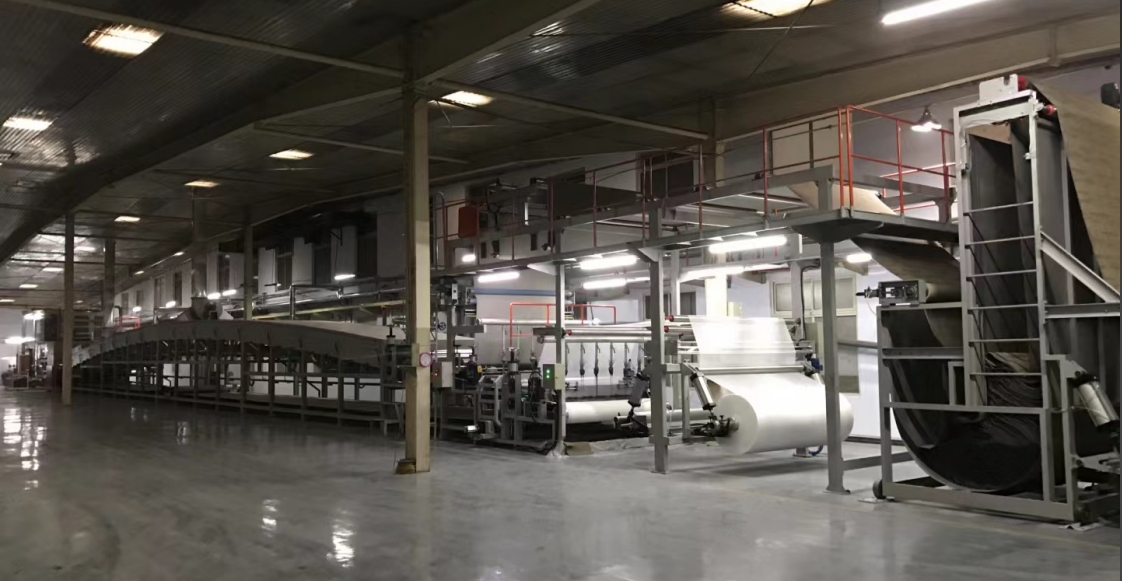
Production line for PVC carpet tiles - backing coating, plastication and automatic cutting for tufted or needle-punched, nylon or polypropylene carpets, producing 50x50, 50x100, 25x100, 100x100 and polygonal tiles.
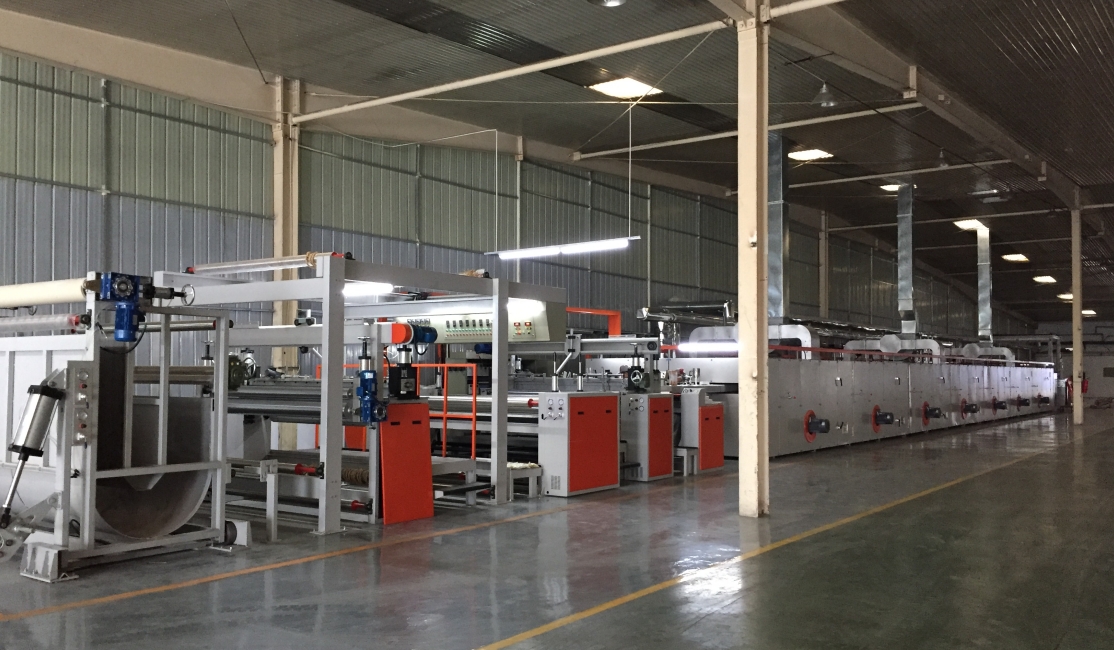
Pre-coating line for woven and tufted carpet backing (pre-coating and drying) to prepare for subsequent PVC / bitumen / TPO coating.
A: TECH on this page: nominal width 200 cm adjustable; machine speed 1–12 m/min; typical running speed 5–7 m/min; oven 100–200℃; cooling 20–60℃ automatic water cooling; main power ≈45 KW (automatic ≈60 KW). Full fields are in the TECH table above.
A: Both modes are published on this page. Slitting suits staged cutting workflows; fully automatic continuous ties coat → cool → cut in one rhythm. Bring target shift output, tile SKUs, and labor plan so we can recommend a mode—do not assume the higher power figure alone decides it.
A: Bitumen/TPO compounds need a controlled cool before cut to limit warp and edge smear. TECH lists cooling 20–60℃ with automatic water cooling as the published band; the setpoint is locked in commissioning against your compound.
A: Public patent CN219723533U describes an asphalt composite coating head for carpet backing. It shows technical direction for bitumen application heads; your delivered head follows the quotation and process brief.
A: No. The published mix is a series tendency. Plant energy, safety, and compound temperature window decide the source in the proposal.
A: Pre-coat (carpet-03) prepares woven/tufted backing before PVC or bitumen/TPO. After tiles are cut, carpet-04 packaging handles turn-over, stacking, and cartoning. Send greige width, compound type, tile SKUs, and carton plan with the inquiry.