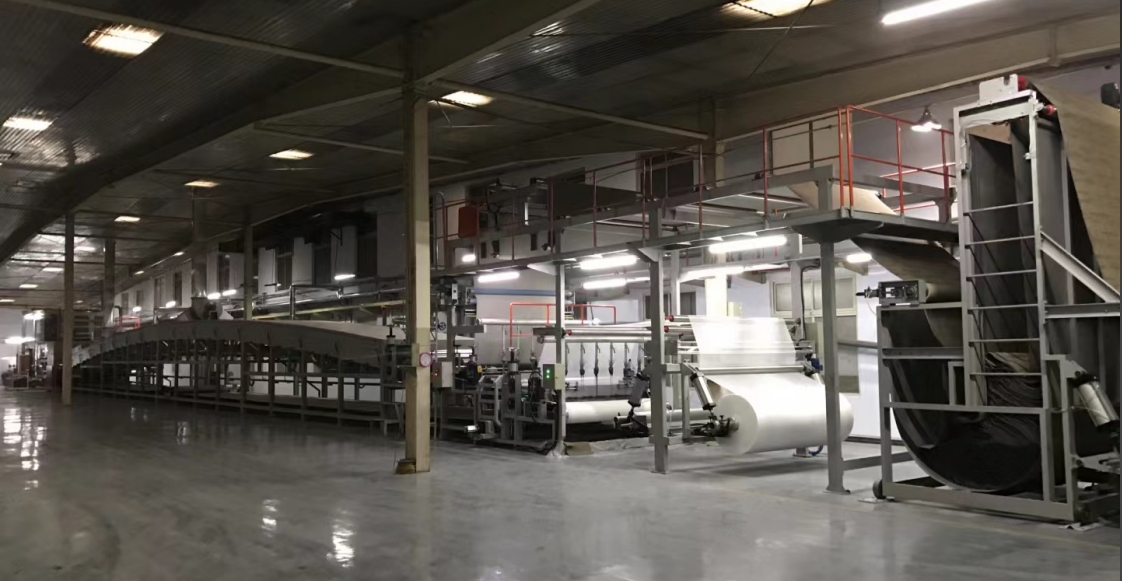
Production line for PVC carpet tiles - backing coating, plastication and automatic cutting for tufted or needle-punched, nylon or polypropylene carpets, producing 50x50, 50x100, 25x100, 100x100 and polygonal tiles.
| Model / series | FH-220 |
|---|---|
| Nominal width | 200cmadjustable |
| Machine speed | 1-12m/min |
| Typical running speed | 5-6m/min |
| Heat source | thermal oil 15%; natural gas 80%; steam 5% |
| Oven | Configured to customer needs |
| Tile sizes | 50x50, 50x100, 25x100, 100x100cm, polygonal |
| Drive | Horizontal Teflon belt conveying |
| Oven temperature | 100-200℃ automatic control |
| Main power | ≈55KW |
Production line for PVC carpet tiles - backing coating, plastication and automatic cutting for tufted or needle-punched, nylon or polypropylene carpets, producing 50x50, 50x100, 25x100, 100x100 and polygonal tiles.
The line coats PVC backing onto tufted or needle-punched nylon or polypropylene carpet, plasticizes the coat, then cuts tiles. Published USE covers 50×50, 50×100, 25×100, 100×100 cm and polygonal formats.
Infeed and horizontal transfer run on a Teflon (PTFE) belt so thick paste and plasticizing stay supported without sticking. Coating weight and knife/head setting affect stiffness, flatness, and cut-edge quality.
Plasticizing uses an oven configured to the order. Published oven band is 100–200℃ with automatic control. Heat source options on this page’s TECH table: thermal oil, natural gas, or steam (series mix shown as percentages—not a mandate to use gas). Cool thoroughly before cutting to limit tile warp; cooling length follows recipe and speed in the proposal.
Model FH-220 is the published PVC tile backing series; factory sub-IDs follow the contract.
Nominal width 200 cm adjustable: check against greige usable width and tile nesting. Machine speed 1–12 m/min is the mechanical band with VFD—not a promise that every paste weight and tile size runs at the top.
Typical running speed 5–6 m/min is the published stable-window example. Oven “configured to customer needs” means chamber count and length are a customization core. Main power ≈55 KW covers the machine frame; external boiler / thermal-oil heater load is on the electrical list.
PVC plasticizing oven directions (publications CN214521400U blanket-belt plasticizing oven; CN208392450U direct-fired PVC-line plasticizing oven): public texts describe oven layouts aimed at even plasticizing of PVC carpet backing. Delivered heat source and chamber count still follow the TECH options and contract—not every drawing.
Electro-hydraulic servo in carpet coating (publication CN206111703U): describes servo control for coating-process motion so head/roll response can track setpoints more tightly during backing. Exact actuators on your order follow the quotation.
These notes summarize public technical directions for overseas buyers. We do not post a full patent wall on the site; a longer list can be shared in discussion. Publication numbers are not a claim of present legal status for every family member.
This machine: PVC coat → plasticize → cut. Choose it when the backing system is PVC.
Bitumen / TPO Carpet Tile Production Line: bitumen or TPO coat → backing → cool → cut; slitting or fully automatic continuous modes are published there.
Pick the chemistry first, then the host. A Carpet Tile Pre-Coating Line usually helps either route. Downstream: Automatic Continuous Cutting Machine (if cutting is separate) and Carpet Tile Automatic Packaging Line.
Usually a fit: nylon/PP tufted or needle-punched greige aimed at PVC-backed tiles; published tile SKUs including polygonal; willingness to lock oven, heat source, and speed window with samples.
Usually another page: bitumen/TPO-only programs (see carpet-02); roll goods without tile cutting; no greige/PVC data yet demanding locked peel or dimensional acceptance values.
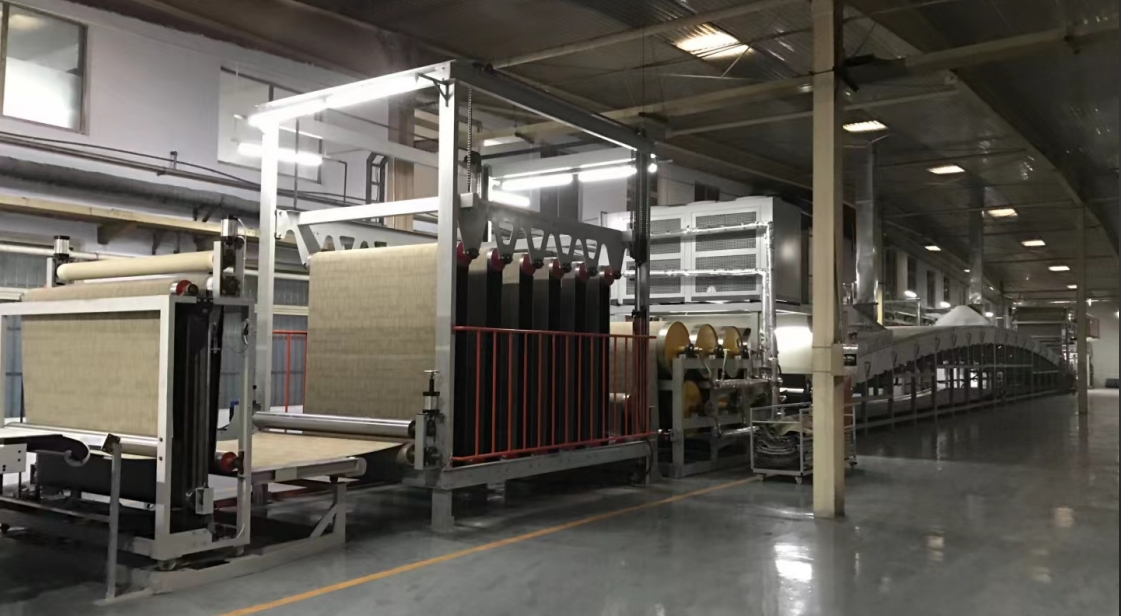
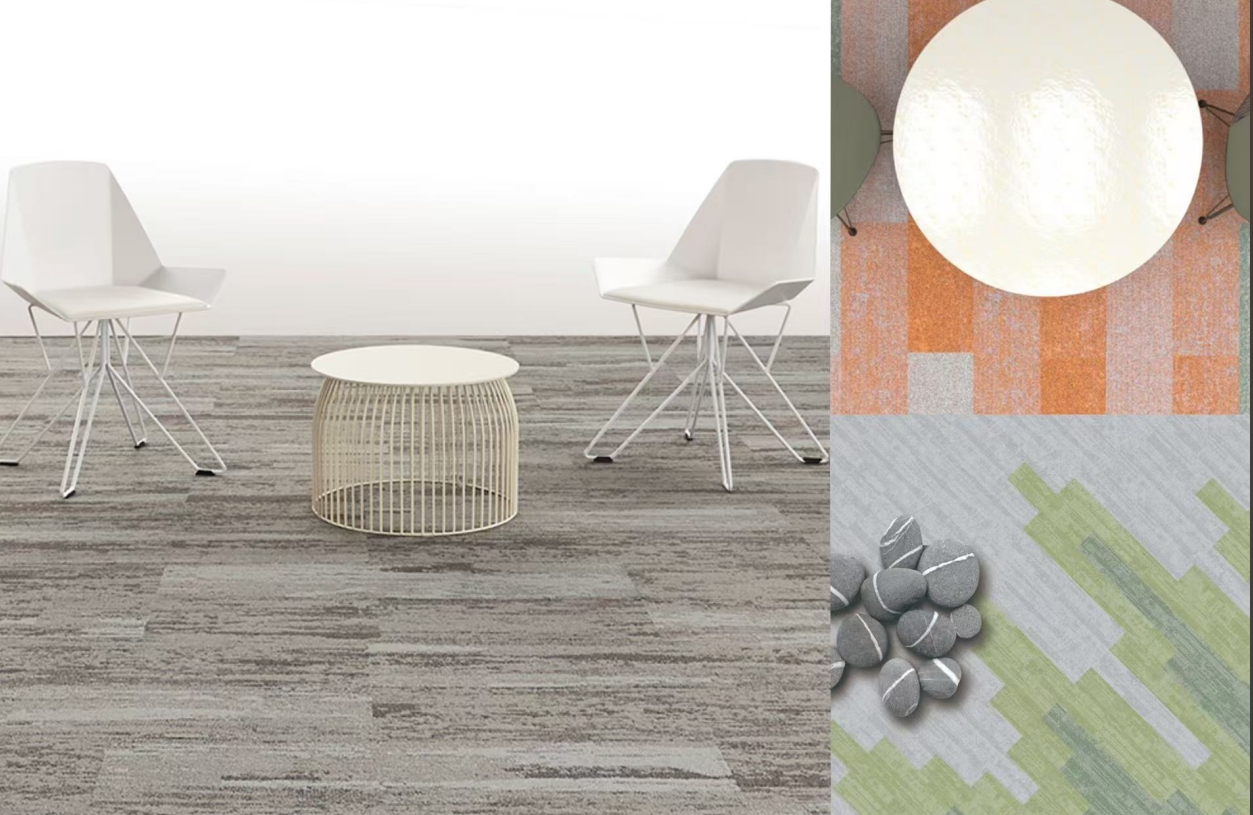
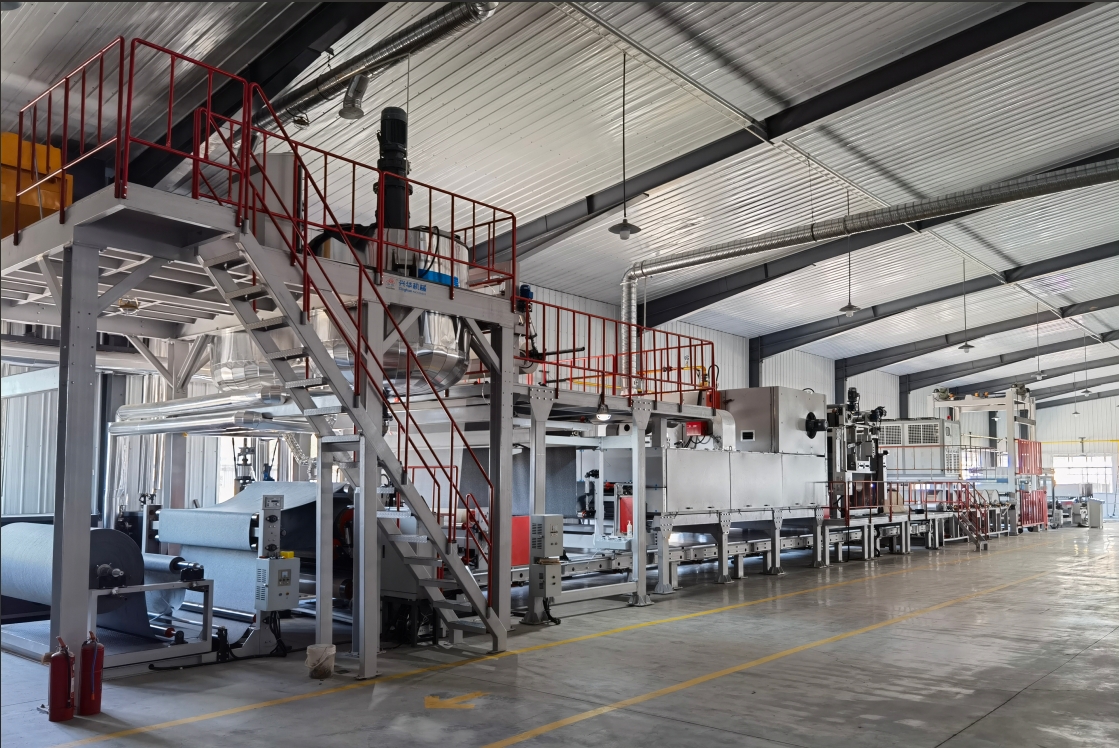
Production line for bitumen / TPO carpet tiles - back coating with bitumen/TPO, backing, cooling and automatic cutting for tufted or needle-punched carpets, available in slitting or fully automatic continuous production.
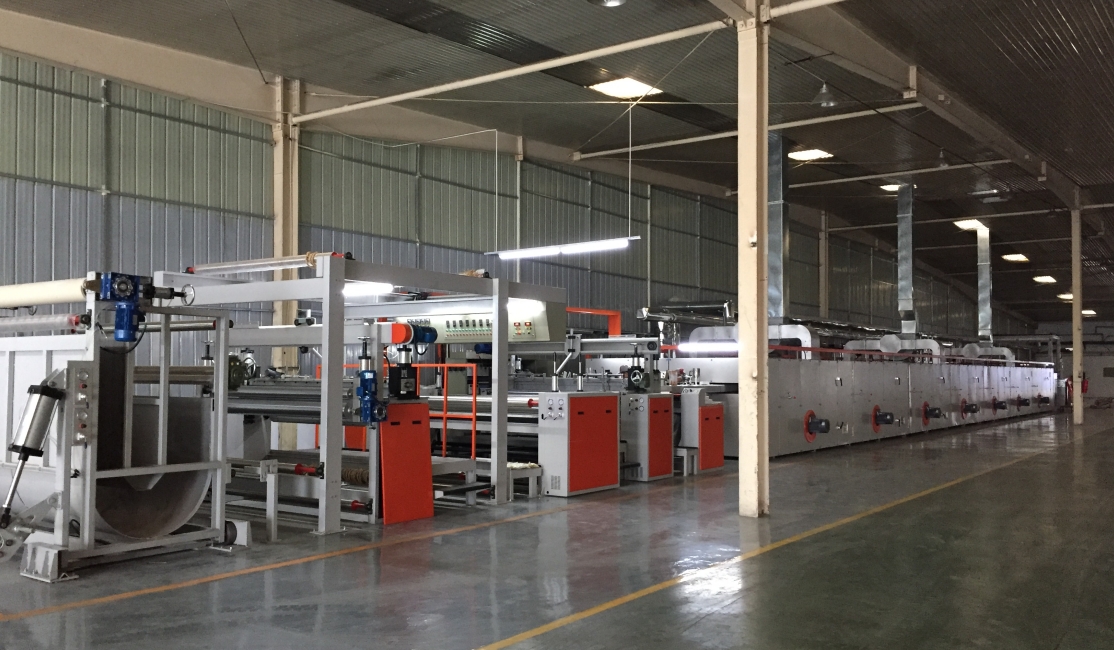
Pre-coating line for woven and tufted carpet backing (pre-coating and drying) to prepare for subsequent PVC / bitumen / TPO coating.
A: TECH on this page: nominal width 200 cm adjustable; machine speed 1–12 m/min; typical running speed 5–6 m/min; main power ≈55 KW; oven 100–200℃ automatic control. Heat-source mix (thermal oil / natural gas / steam) is a series tendency, not a forced choice. Full fields are in the TECH table—mechanical range is not a promise that every paste and tile runs at the top.
A: Tile PVC coating needs steady support and an easy-release face under thick paste and plasticizing. This page’s TECH lists horizontal Teflon belt conveying. Rail-chain drives appear on other coating models; they serve different product forms—neither is “more advanced” in the abstract.
A: No. The published mix (thermal oil 15%; natural gas 80%; steam 5%) shows common delivery tendency for this series. Match plant energy and safety first; oven design follows the chosen source in the proposal.
A: Polygonal formats need different cutting paths/tooling and registration. If polygons are a primary SKU, define them at order time—not after start-up. Published sizes on this page include 50×50, 50×100, 25×100, 100×100 cm and polygonal.
A: Public texts CN214521400U and CN208392450U describe plasticizing-oven directions for PVC carpet backing (belt-style and direct-fired layouts). Your chambers, fuel, and length still follow TECH “configured to customer needs” and the contract.
A: From a process-stability view, pre-coat reduces fiber shed and uneven adhesion risk on the main coat—especially for new plants. If incoming greige already has a qualified pre-coat, the host can lead, but write pre-coat quality into incoming standards. See Carpet Tile Pre-Coating Line.